News

MAThread Patent Thread Rolling Dies: Selection Criteria

Railway Rivet Flat Thread Rolling Dies Guide

Guide to Wooden Screw with Scoopes Flat Thread Rolling Dies
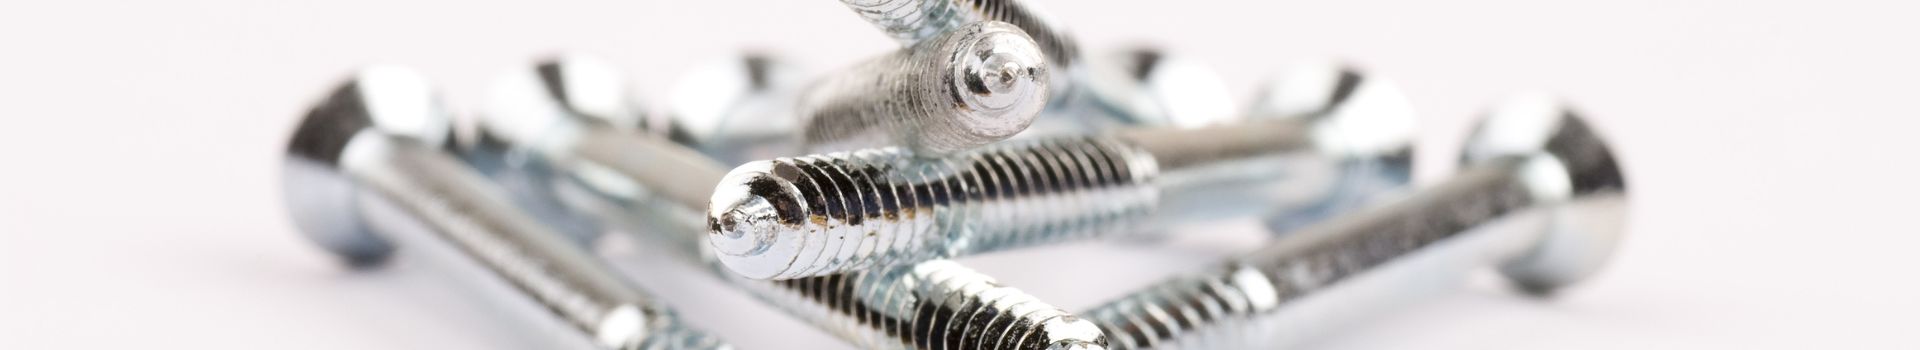
Wood screws designed for fast penetration into dense timber depend on more than a sharp point—they rely on precisely formed threads that grip, cut, and resist failure under load. Flat thread rolling dies for scooped-point wood screws are specialized cold-forming tools that shape these aggressive profiles at industrial speeds, often reaching several hundred parts per minute when matched to the right machine and blank. This guide explains how the dies work, why the scooped or fluted point must be coordinated with the rolling process, and how cold-formed threads can improve strength, durability, and installation performance compared with cut-thread alternatives.

Serrated Screw Flat Thread Rolling Dies: Buyer Specifications
Selecting the optimal die configuration dictates both the quality of the finished fastener and the overall economic efficiency of the production run. Before evaluating metallurgy, buyers must first verify machine compatibility by confirming standard die blank dimensions—such as DIN specifications or machine-specific length, width, and height requirements. Procurement engineers must then evaluate metallurgical properties alongside geometric tolerances to ensure the tooling withstands the severe cyclical stresses of cold forming.

Gimlet Screw Flat Thread Rolling Dies: Buyer Specifications
In high-volume screw manufacturing, a small error at the point can become a large production problem. Forming self-tapping, sheet metal, and wood screws requires dies that do more than roll a uniform thread—they must also forge a sharp gimlet tip that penetrates material reliably without pre-drilling. At machine speeds of 300 to 800 parts per minute, die material, hardness, coating, geometry, lubrication, and blank preparation all influence output, tool life, and fastener performance. This guide explains the key buying specifications engineers should review before ordering flat thread rolling dies, with a focus on durability, dimensional accuracy, point quality, and stable high-speed production.

MAThread® Thread Rolling Die for Bolt Production
Cross-threading is a small defect with outsized consequences: one misstarted bolt can stall a robotic cell, damage mating threads, and create costly rework in seconds. MAThread® rolling die technology addresses that risk at the source by forming a controlled self-aligning lead-in on the bolt tip during thread rolling. This article explains how the geometry works, how it differs from conventional rolled threads, and where it delivers the greatest production value—from automotive and heavy truck assembly to aerospace fastening. It also highlights practical specification factors, including die steel selection, coatings, mating-hole quality, material ductility, and compatibility with secondary thread treatments.

How to Choose a Circular Thread Rolling Die for Precision Applications
In precision manufacturing, a thread is not just a fastening feature—it is often a load-bearing, fatigue-critical surface. The wrong rolling die can turn a stable production run into a costly source of pitch errors, premature wear, scrap, and machine downtime. Circular thread rolling dies are valued because they form threads through cold deformation, preserving grain flow and improving mechanical performance compared with cutting. But selecting the right die requires more than matching a nominal thread size. Material grade, hardness, coating, tooth geometry, machine setup, and target production volume all influence results. This guide explains the practical selection factors that help engineers achieve consistent, high-strength threads in demanding applications.

Circular Thread Rolling Die Selection for Precision Fasteners
Precision fasteners earn their performance at the thread root, where geometry, material flow, and residual stress determine whether a part survives vibration, fatigue, and repeated loading. Selecting the right circular thread rolling die is therefore more than a tooling purchase; it is an engineering decision that affects dimensional accuracy, die life, surface finish, and final fastener strength. This article explains how to define die requirements around blank diameter, thread profile, rolling method, material hardness, heat treatment, coatings, and machine interface details. With tolerances that may approach ±0.0005 inches in demanding applications, small specification errors can create costly scrap, premature tool failure, or fasteners that miss critical performance targets.

Circular Thread Rolling Die Selection for Precision Fastener Manufacturing
In precision fastener production, the right rolling tool is not a minor purchasing detail—it is a direct driver of thread accuracy, uptime, and cost per part. Circular dies must survive heavy cyclic loading, often in the 15-30 ton range, while holding tight pitch diameter tolerances at high production speeds. A poor specification can quickly turn into scrap, unplanned downtime, and weakened joint performance. This guide explains how die geometry, tool steel, hardness, coatings, and machine compatibility influence thread quality and production economics, helping engineers and buyers make a more reliable selection for high-volume cold-forming operations.

Circular Thread Rolling Die Selection for Precision Fasteners
Fastener performance often depends less on the bolt drawing than on the tooling that forms its threads. In cold forming, cylindrical thread rolling tooling must control extreme radial loads while shaping metal without cutting away grain structure. The result can be stronger threads, better surface finish, and faster output—but only when die geometry, coating, material, alignment, and lubrication are specified correctly. This article explains where circular dies outperform flat or planetary options, which dimensional details determine thread compliance, and why small decisions such as coating allowance or chamfer design can decide whether a production run meets aerospace-grade tolerance or creates costly assembly failures.