

Wood screws designed for fast penetration into dense timber depend on more than a sharp point—they rely on precisely formed threads that grip, cut, and resist failure under load. Flat thread rolling dies for scooped-point wood screws are specialized cold-forming tools that shape these aggressive profiles at industrial speeds, often reaching several hundred parts per minute when matched to the right machine and blank. This guide explains how the dies work, why the scooped or fluted point must be coordinated with the rolling process, and how cold-formed threads can improve strength, durability, and installation performance compared with cut-thread alternatives.
Understanding Wooden Screw with Scoopes Flat Thread Rolling Dies
Flat thread rolling dies engineered for wood screws with scooped points represent a specialized segment of cold-forming tooling. These precision instruments are critical for manufacturing fasteners that require aggressive thread profiles, ensuring efficient penetration into dense timber without the need for pre-drilling. Mastering the application of these dies is essential for optimizing fastener production.
Product definition and core applications
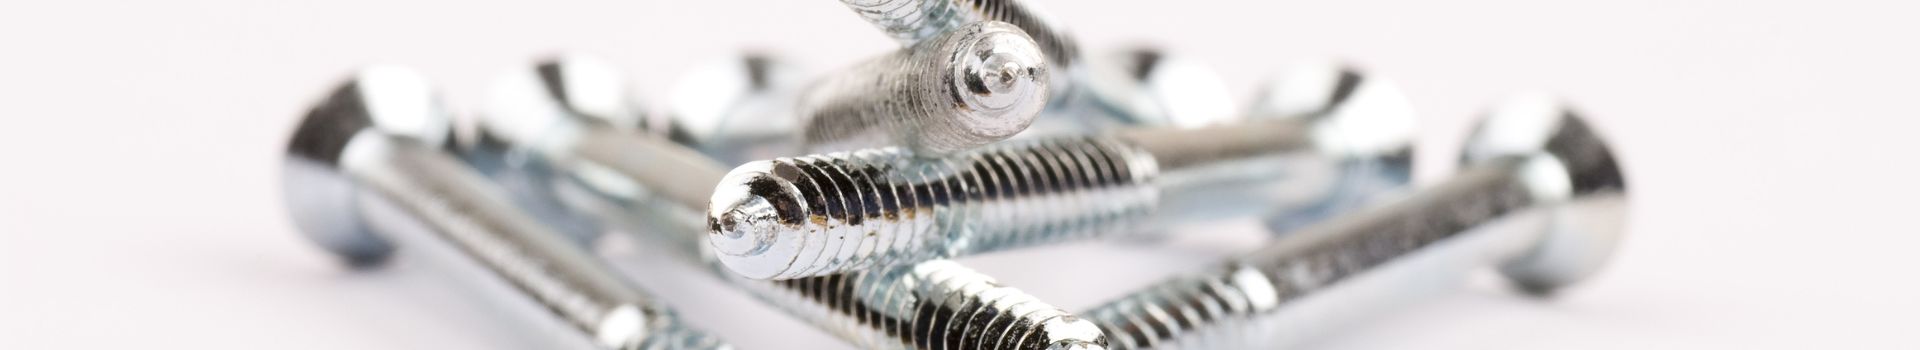
A wood screw with a scooped point features a specialized flute at its tip designed to capture and evacuate wood debris during installation. While sometimes used interchangeably in general contexts, it is important to distinguish general scooped or auger points from the Type 17 point, which refers to a specific, standardized cutting flute geometry. The flat thread rolling dies utilized to produce these fasteners consist of two machined rectangular plates: one stationary and one reciprocating. As the unthreaded, pre-pointed blank is rolled between the plates under mechanical pressure, the die's precision-ground ridges displace the metal to form the deep, widely spaced threads characteristic of wood screws. It is important to note that the scooped point itself is typically created in a separate pointing or gashing operation prior to rolling; the thread rolling die must be precisely matched to this pre-formed blank.
These dies are indispensable in industrial environments supplying the decking, cabinetry, and structural timber sectors. Producing these asymmetric thread profiles requires dies with specific slip and grip zones to prevent the blank from skidding during the initial rotation.
How flat thread rolling dies shape screw performance
The application of flat thread rolling dies fundamentally enhances the mechanical properties of the finished wood screw. Because the cold-forming process displaces instead of severing the material's internal grain structure, the resulting fasteners exhibit increased tensile and shear strength compared to machined or cut alternatives. The compressive forces applied during rolling also work-harden the thread crests, improving the screw's overall durability and drive performance.
Furthermore, the precise calibration of the dies ensures the threads align correctly with the pre-formed scooped point, which directly impacts the screw's ability to prevent wood splitting during rapid installation. Modern thread rolling machines utilizing these specialized dies operate at high velocities. Depending on the blank diameter, material composition, and machine capabilities, production rates can reach several hundred parts per minute, maximizing throughput while maintaining strict geometric tolerances.
Key Specifications and Performance Comparisons

Selecting the optimal flat thread rolling die requires an evaluation of technical parameters, dimensional compatibility, and metallurgical properties. Industrial buyers and production engineers must balance tool longevity against initial procurement costs to maximize overall production efficiency and minimize machine downtime. When comparing manufacturing methods, flat thread rolling dies offer distinct advantages over cut-thread or cylindrical-die processes for wood screw production. Unlike thread cutting, which removes material and interrupts the grain structure, flat rolling cold-forms the blank for superior shear strength and faster cycle times. Compared to cylindrical dies, flat dies are generally more cost-effective and efficient for high-volume, continuous runs of asymmetric wood screw profiles.
Technical specifications to compare
Compatibility between the thread rolling machine and the die set is governed by strict dimensional specifications, which are machine-specific rather than universal standards. Engineers must evaluate the die length, width, and thickness, alongside the maximum thread length and blank diameter capacities. The thread profile itself—incorporating the asymmetric pitch and sharp crests required for gripping wood fibers—must be flawlessly ground into the die face to avoid material fatigue during the rolling stroke.
Note: The following table provides illustrative example data; die dimensions and stroke capacities vary significantly by machine manufacturer and are not universal standards.
| Machine Capacity Profile | Max Thread Length (mm) | Blank Diameter Range (mm) | Typical Machine Stroke (mm) |
|---|---|---|---|
| Small Frame | 40 | 2.0 - 4.0 | 100 |
| Medium Frame | 65 | 3.0 - 5.0 | 125 |
| Large Frame | 80 | 4.0 - 6.0 | 150 |
Selecting the correct dimensional specification ensures the moving die completes a sufficient number of rotations over the blank. As a rule of thumb, a minimum of three full rotations is typically required to fully form the deep thread profile without inducing skidding or causing premature wear on the die's entry zone, though exact requirements depend heavily on thread pitch, blank diameter, and machine kinematics. Die performance also relies on the blank material and whether the machine stroke is adequately sized for the fastener.
Material, hardness, and durability trade-offs
The metallurgical composition of the die dictates its operational lifespan and resistance to wear under extreme cold-forming pressures. Standard dies are frequently machined from D2 tool steel and heat-treated to a hardness of HRC 58-60. This provides a cost-effective baseline durability that is generally sufficient for rolling standard low-carbon steel screw blanks.
For continuous production, or when rolling harder alloy blanks, upgrading to High-Speed Steel (HSS) such as M2 or advanced matrix tool steels like DC53 is preferred. While these premium materials require a higher initial tooling investment, they achieve superior hardness levels of HRC 62-65, which significantly reduces the risk of thread crest chipping under heavy loads. Implementing advanced surface treatments, such as Titanium Nitride (TiN) physical vapor deposition (PVD) coating or gas nitriding, further alters the tooling economics. Although coatings add upfront expense, they lower the coefficient of friction and can drastically extend the die's lifecycle before professional regrinding becomes necessary.
Buyer Qualification and Sourcing Guidance
Procuring precision tooling for scooped wood screws necessitates a systematic approach to supplier validation and quality assurance. Buyers must establish qualification protocols to mitigate the risks of production downtime, inconsistent thread geometries, and unacceptable fastener defect rates.
Supplier qualification and sample approval steps
The supplier qualification process must begin with an audit of the manufacturer's machining and grinding capabilities. Premium flat thread rolling dies require advanced CNC profile grinding equipment capable of maintaining dimensional tolerances of ±0.01 mm or better.
Key Takeaways
- Use flat thread rolling dies matched to the pre-formed scooped blank to prevent skidding and ensure correct thread-to-point alignment.
- Create the scooped or fluted point before rolling, because flat dies primarily form the thread rather than the cutting tip.
- Choose thread rolling over thread cutting when higher tensile strength, shear strength, and work-hardened thread crests are required.
- Specify dies with proper slip and grip zones for aggressive wood screw profiles to stabilize blank rotation during high-speed production.
- Evaluate die selection by balancing dimensional compatibility, metallurgy, tool life, procurement cost, and expected machine downtime.
Frequently Asked Questions
What are flat thread rolling dies used for in wood screw production?
They cold-form deep, widely spaced threads on pre-pointed screw blanks, creating strong wood screws suited for decking, cabinetry, and structural timber applications.
Do the dies create the scooped point on the screw?
Usually no. The scooped or fluted point is typically made in a separate pointing or gashing operation before thread rolling begins.
How is a scooped point different from a Type 17 point?
A scooped point is a general debris-clearing tip style, while Type 17 refers to a specific standardized cutting flute geometry used on certain wood screws.
Why use thread rolling instead of thread cutting?
Thread rolling displaces metal rather than removing it, preserving grain flow and improving tensile strength, shear strength, and thread durability.
What makes die alignment important for scooped-point wood screws?
The die profile must match the pre-formed blank so the thread starts correctly behind the point, supporting clean penetration and reducing wood splitting.