

MAThread Patent Thread Rolling Dies: Selection Criteria

In high-speed fastener production, a small misalignment at installation can become an expensive problem: stripped holes, torque spikes, scrap, and slowed assembly lines. MAThread® fasteners address this by using a patented self-aligning thread point, but producing that geometry requires more than a standard rolling tool. Manufacturers must evaluate die authorization, machine compatibility, blank hardness, profile accuracy, and long-term wear resistance before committing to production. This guide explains how MAThread® thread rolling dies work, where their application limits matter, and what purchasing teams should verify when selecting a precision tooling partner such as Wanying Henghui for custom high-volume fastener manufacturing.
Understanding MAThread Patent Thread Rolling Dies
MAThread technology has significantly improved high-volume assembly environments by reducing cross-threading during fastener installation. Producing these specialized fasteners requires precision thread rolling dies engineered to form the patented transitional geometry. Importantly, because MAThread is a patented technology, die geometry and licensing are strictly controlled by the patent holder. Buyers must confirm authorized sourcing channels rather than expect multiple competing die designs. For fastener manufacturers, understanding the specific mechanical interactions of MAThread profiles is critical before specifying the rolling dies required for high-speed production. The dies must not only forge the standard helical thread but also shape the corrective point in a single, continuous stroke.
Key Definitions and Application Limits
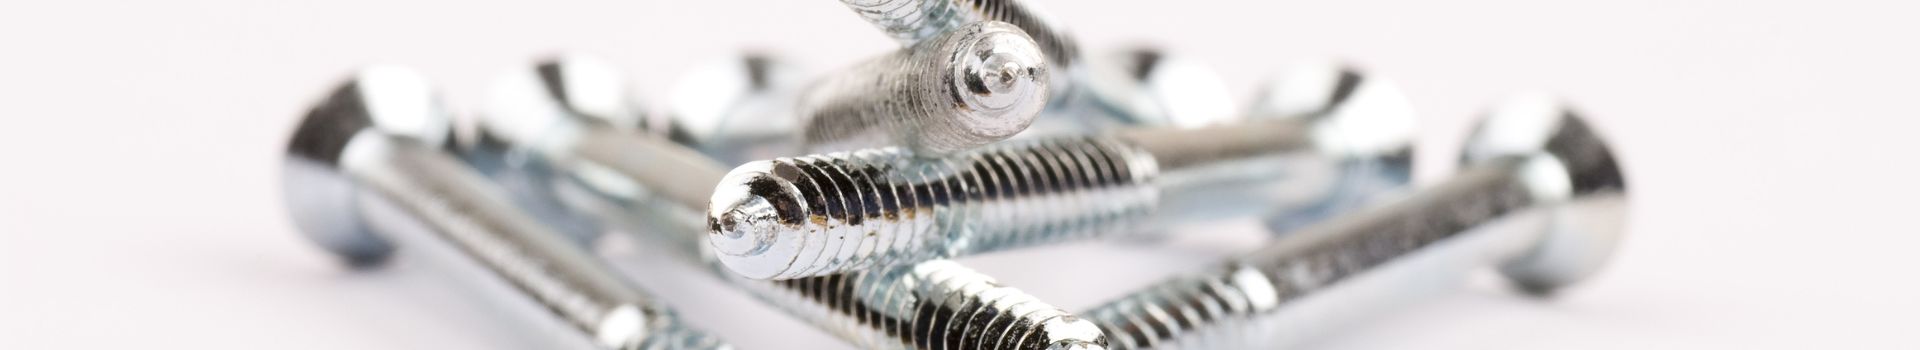
The MAThread design features a specialized dog-point or "p-point" with a cam-like transitional thread that guides misaligned fasteners into the correct helical path. Thread rolling dies designed for this patent must incorporate a precise runout and blank-taper angle to form the anti-cross-threading feature without fracturing the steel grain structure of the blank. Flat, planetary, and cylindrical die configurations can be adapted for this purpose, provided the entry ramp is customized and the die supplier supports the specific configuration. Application limits for standard MAThread rolling dies encompass fastener sizes ranging from M4 to M24. Furthermore, the blank wire material being rolled must remain below a hardness threshold of 35 to 40 HRC. Exceeding this hardness limit prevents adequate material flow into the specialized root geometry of the die and increases the risk of tool failure.
Impact on Assembly Performance
Implementing MAThread fasteners yields a measurable impact on assembly line efficiency, which offsets the premium cost of the specialized rolling dies. The unique thread profile corrects off-angle installations of up to 15 degrees, automatically aligning the fastener with the internal female thread before full engagement occurs. This mechanical correction eliminates assembly torque spikes and mitigates the risk of stripped tapped holes in engine blocks and chassis castings. Consequently, automotive and aerospace manufacturers report significant reductions in installation-related scrap rates. Additionally, this self-aligning capability lowers the ergonomic strain on operators utilizing heavy pneumatic or DC electric torque tools, supporting faster takt times and justifying the investment in high-precision rolling dies.
Selecting the Right Thread Rolling Die

Specifying the correct thread rolling die for MAThread production requires an evaluation of metallurgical properties, manufacturing tolerances, and the specific dynamics of the cold forming process. Buyers must ensure compatibility with the existing rolling machine by verifying die dimensions, pass configurations, and tangential versus thru-feed setups. Additionally, evaluating required setup times, changeover considerations, and the regrind or rework service life of the dies is essential. The chosen die must withstand immense compressive forces while maintaining the intricate patented geometry over hundreds of thousands of threading cycles without significant wear.
Material, Coating, Geometry, and Tolerance
The selection of die material and subsequent surface treatment influences tool longevity and overall thread quality. Common substrates include cold-work tool steels like D2 and DC53, as well as high-speed steels such as M2. To further enhance wear resistance and prevent galling, physical vapor deposition (PVD) coatings like Titanium Nitride (TiN) or Titanium Carbonitride (TiCN) are applied to reduce friction during the high-speed rolling process. Tolerances must be tightly controlled, requiring the dies to consistently produce fasteners within a standard 6g tolerance class to ensure proper mating with internal threads. Maintaining a fine surface finish, targeted around Ra 0.4 µm, on the die threads helps ensure smooth material flow and prevents micro-fractures in the fastener blank.
The following table provides illustrative, typical ranges for die materials, coatings, and expected tool life:
| Die Material | Typical Coating | Hardness (HRC) | Illustrative Tool Life (Pieces) |
|---|---|---|---|
| D2 Tool Steel | Uncoated / Nitrided | 58 - 60 | 100,000 - 150,000 |
| M2 High-Speed Steel | TiN | 62 - 64 | 250,000 - 350,000 |
| DC53 Cold-Work Die Steel | TiCN | 60 - 62 | 400,000 - 500,000 |
Supplier Capability Evaluation
Evaluating a supplier's manufacturing capability extends beyond analyzing published metallurgical data. The die manufacturer must possess the explicit technical capability to grind the proprietary cam profile accurately using advanced CNC thread grinders. Substandard machining will result in incorrect thread geometry and failed fastener alignment. Procurement engineers should verify ISO 9001 or IATF 16949 certifications to ensure the presence of appropriate quality management systems. Additionally, assessing logistical parameters is vital for supply chain stability. Typical lead times for custom-ground MAThread dies range from 4 to 8 weeks, with Minimum Order Quantities (MOQs) set between 3 to 5 sets depending on the complexity of the die configuration.
Final Approval and Purchasing Decision
The transition from initial supplier selection to active fastener production relies on a structured validation protocol. Because MAThread fasteners are utilized in automotive and heavy industrial applications, the rolling dies must consistently produce accurate transitional threads throughout their lifecycle.
Validation Steps Before Approval
Prior to authorizing full-scale production runs, engineering teams mandate a First Article Inspection (FAI) followed by a formal Production Part Approval Process (PPAP). A PPAP submission, complete with Control Plans and a Failure Mode and Effects Analysis (FMEA), ensures the supplier has anticipated and mitigated potential manufacturing variations. This validation phase involves rolling a pilot batch to evaluate die performance under standard operating speeds and realistic thermal conditions. Quality control personnel utilize optical comparators, profile projectors, and specialized MAThread ring gauges to verify that the dog-point aligns with the patented dimensional specifications. Deviations in the transitional pitch compromise the anti-cross-threading properties, making pilot batch validation a critical step in the supplier approval pipeline.
Quality Risk Decision Matrix
To consolidate validation data and finalize the purchasing decision, procurement teams should employ a quality risk decision matrix. The following example matrix illustrates suggested weightings to calculate the total cost of ownership (TCO) and overall supplier viability:
| Evaluation Criteria | Suggested Weighting | Scoring Metric (1-5) |
|---|---|---|
| Die Life per Piece & Durability | 30% | Expected cycles |
Key Takeaways
- Verify MAThread® licensing and authorized die geometry before purchasing because the transitional thread profile is patent-controlled.
- Keep blank material hardness below 35 to 40 HRC to ensure proper cold flow into the specialized root and point geometry.
- Match the die configuration to the rolling machine by checking die dimensions, pass design, and tangential or thru-feed requirements.
- Use MAThread® fasteners where assembly misalignment is costly, as the profile can correct off-angle installation up to about 15 degrees.
- Evaluate die material, coating, tolerance control, and regrind service life to protect thread quality over high-volume production runs.
Frequently Asked Questions
What makes MAThread® thread rolling dies different from standard dies?
MAThread® dies form both the normal thread and the patented self-aligning transitional point in one rolling process, requiring precise geometry, runout control, and authorized design specifications.
Can any supplier manufacture MAThread® rolling dies?
No. Because MAThread® is patented, buyers should verify licensing, authorization, and geometry compliance before sourcing dies, rather than treating them as generic thread rolling tools.
What fastener sizes are commonly supported by MAThread® dies?
Standard MAThread® die applications typically cover fastener sizes from M4 to M24, depending on the rolling machine, blank design, material, and production requirements.
What blank hardness is suitable for MAThread® rolling?
The blank material should generally remain below 35 to 40 HRC so it can flow properly into the specialized die geometry without causing poor thread formation or tool damage.
Why are MAThread® fasteners valuable in automotive and aerospace assembly?
They can correct off-angle installation up to about 15 degrees, helping reduce cross-threading, torque spikes, stripped holes, scrap, and operator strain in high-volume assembly lines.